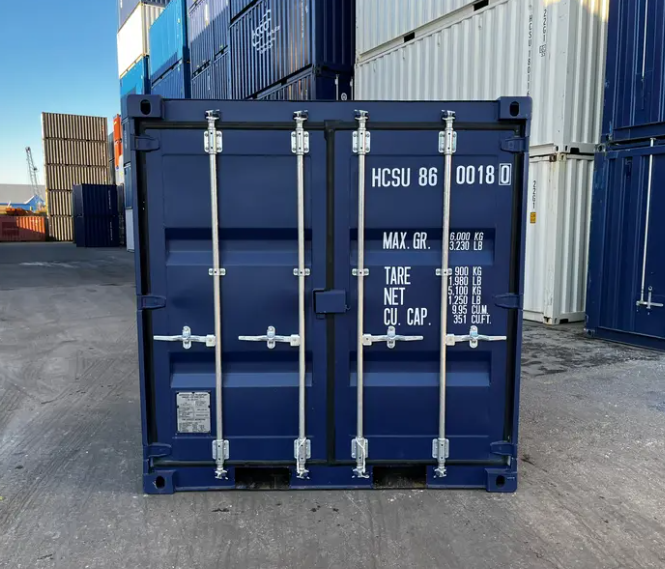
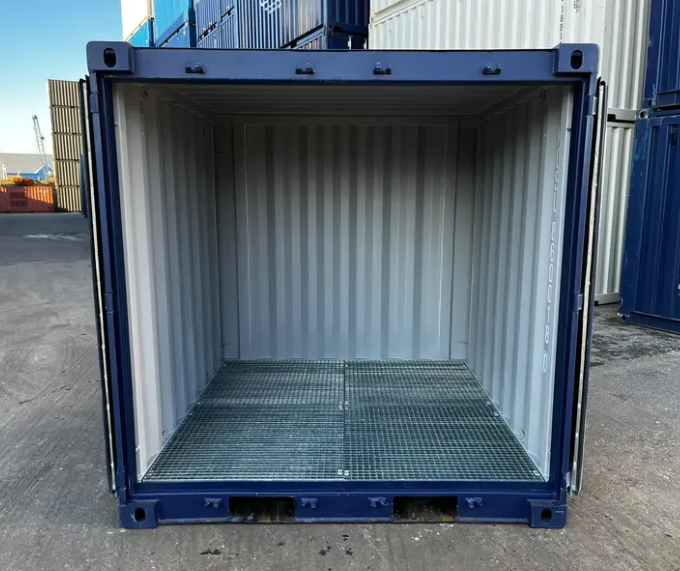
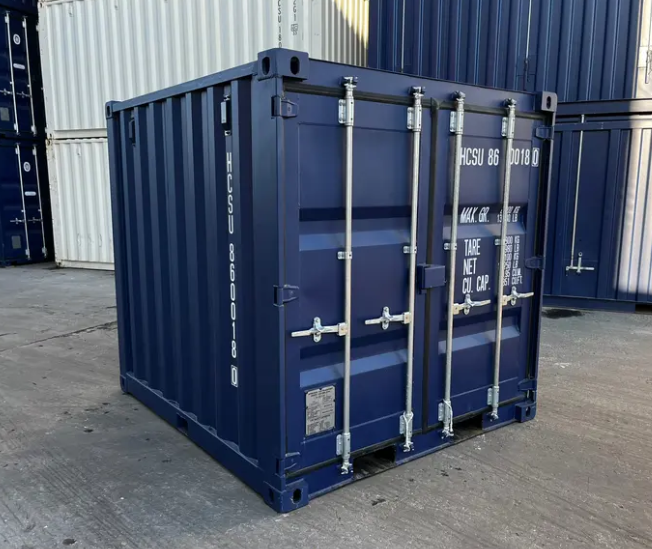
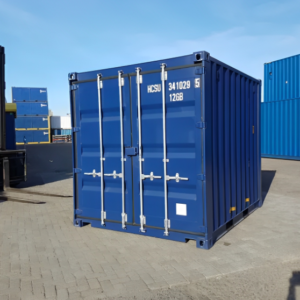
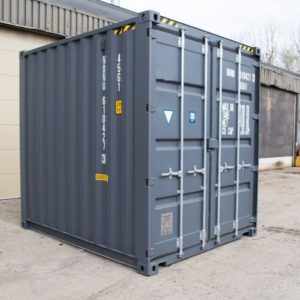
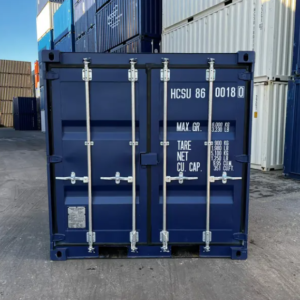
The 8ft Drip-Tray Container is designed specifically for environmental compliance and safe site storage of oils, lubricants, fuels, and chemical drums. Featuring a fully welded, liquid-tight retention sump beneath the walk surface, any accidental spills or leaks are contained immediately before reaching the ground.
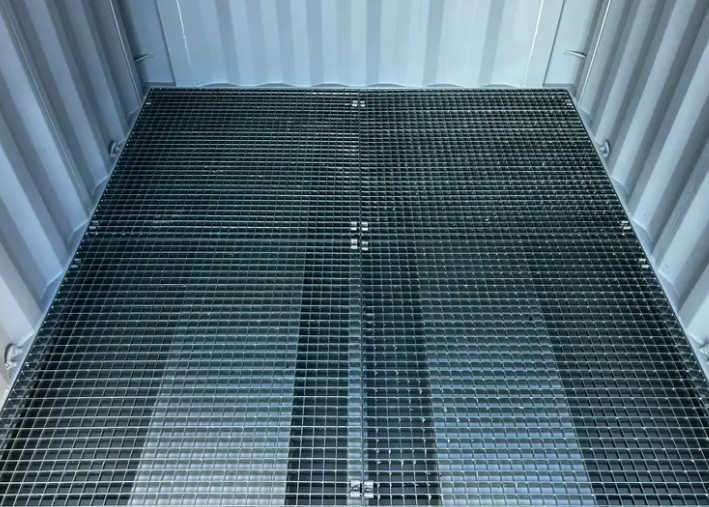
Constructed from heavy-gauge Cor-Ten steel, this container features a removable, hot-dip galvanized steel mesh floor capable of supporting heavy point-loads like full chemical drums and machinery. Double end doors with multi-pocket rubber seals and double locking bars keep contents completely wind and watertight while protecting assets with an integrated lockbox. Built-in forklift pockets allow effortless repositioning across job sites, industrial plants, and agricultural facilities.
Key Features & Specs
-
Integrated Spill Retention Sump: Fully welded floor basin holds liquid spills, protecting surrounding soil and groundwater.
-
Galvanized Mesh Flooring: Removable heavy-duty steel grid supports high weight capacities and allows fast washdowns and cleaning.
-
Weatherproof & Secure: Wind and watertight Cor-Ten steel body with heavy-duty locking mechanisms and lockbox protection.
-
Site Mobility: Factory-fitted with forklift pockets for fast transport and positioning via forklift or telehandler.
Specifications
-
External Dimensions: 8′ L x 7’1″ W x 7’6″ H (2,438 mm x 2,200 mm x 2,260 mm)
-
Internal Dimensions: ~7’6″ L x 6’8″ W x 6’9″ H (~2,280 mm x 2,040 mm x 2,060 mm)
-
Flooring: Removable hot-dip galvanized steel grid over a liquid-tight steel sump
-
Sump Retention Capacity: ~100 – 150 Gallons (400 – 600 Liters)
-
Tare Weight: ~2,100 – 2,300 lbs (~950 – 1,050 kg)
-
Max Payload: ~11,000 lbs (~5,000 kg)
Reviews
There are no reviews yet.